Thermoform Packaging Design: How to Protect Products and Win Shelf Appeal
How to design thermoform blister and clamshell packs that protect products in transit and sell on the hook, from cavity shape to sheet and testing.
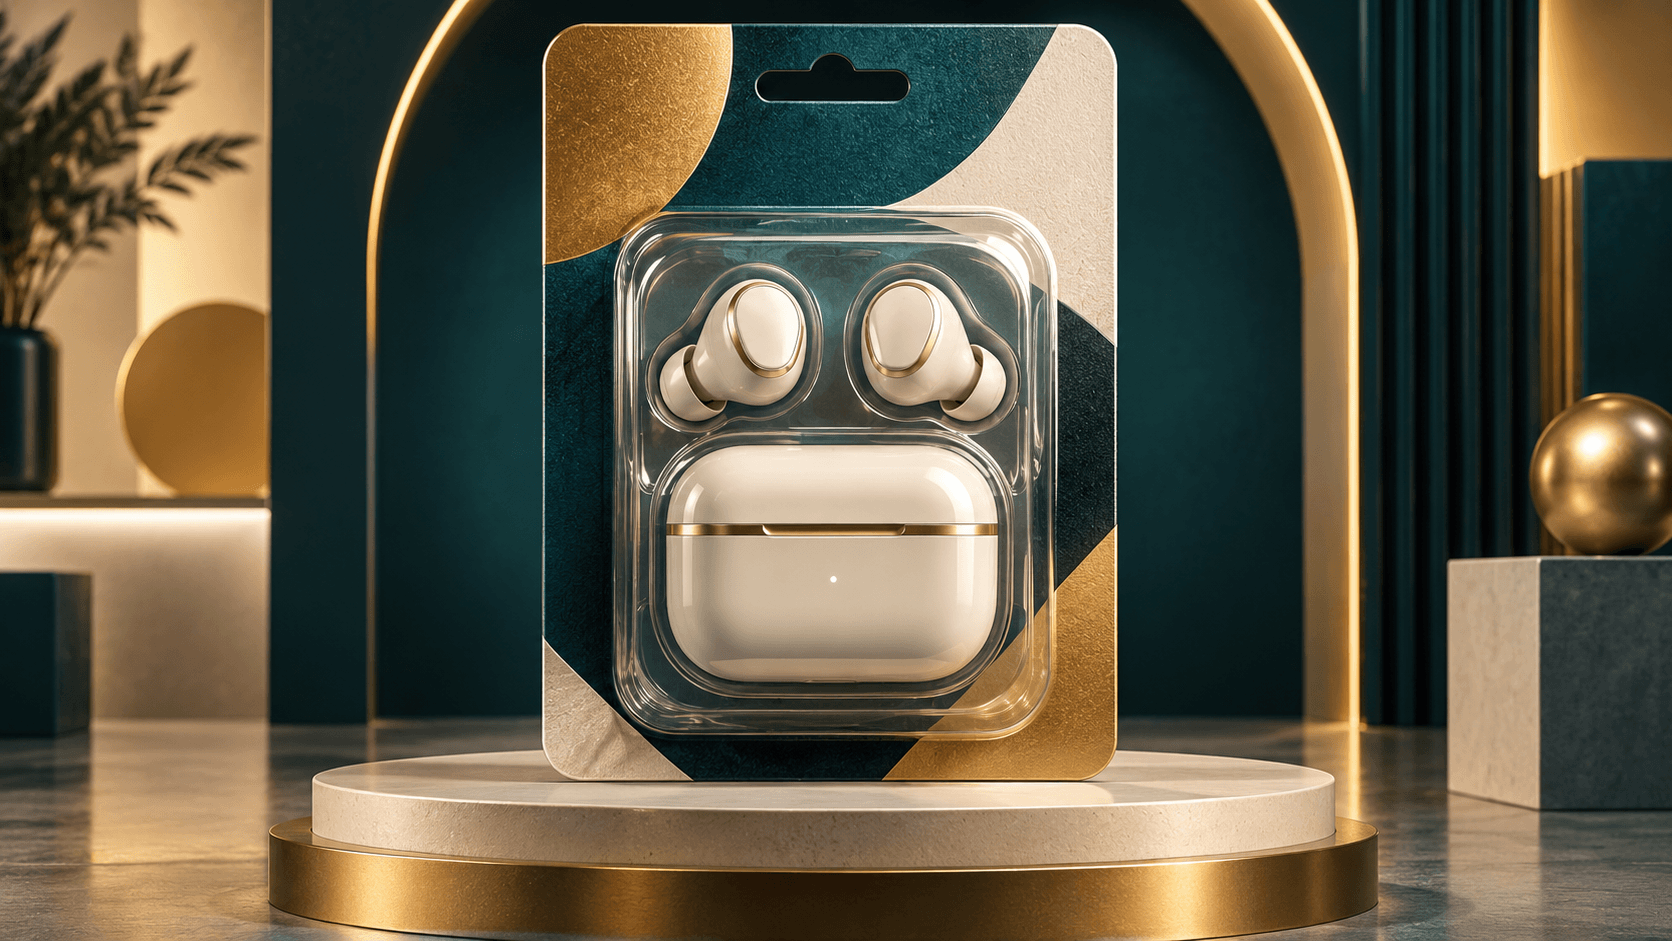
Good thermoform packaging design does not force a choice between product protection and shelf appeal. The same three decisions drive both: the shape of the cavity, the plastic sheet, and the way the pack closes. Get them right before tooling and the pack ships without damage, hangs straight on the hook and sells the product through clear plastic. Get them wrong and you pay twice, once in returns and again for a new tool.
This guide is for brand owners, product managers and packaging buyers who brief a thermoformer rather than run the forming line themselves. It covers formats, cavity design, materials, transit testing, ecommerce and marketplace rules, cost drivers and the new recyclability rules for clear plastic retail packs.
In short:
- Design the cavity outward from the product’s fragile points and treat it as a cradle that stops movement.
- Specify a minimum wall thickness at the deepest corners, not just the starting sheet gauge.
- PET and RPET lead on clarity and recycling, PVC and PETG are easier to seal, and PP suits chemicals and impact.
- Match the backer card’s heat-seal coating to the sheet, or the blister will peel.
- Prove the design with ISTA transit tests on real product, then hang sealed packs on a hook for several days.
- If the product also sells online, check marketplace packaging rules before tooling, because some programs exclude blister packs and welded clamshells.
Table of contents
- What Is Thermoform Packaging?
- Start With the Product’s Weak Points
- Design the Cavity: Draft, Radii and Draw Depth
- Choose the Sheet: PET, RPET, PETG, PVC or PP
- Turn Protection Into Shelf Presence
- Build Security In From the Tool
- Prototype, Then Prove It With Transit Testing
- Selling Online: When a Retail Pack Ships in a Parcel
- Common Thermoform Packaging Failures and How to Fix Them
- What Drives Thermoform Packaging Cost
- Recyclability and the EU PPWR
- What to Put in Your Thermoformer Brief
- PET or PVC? Blister or Clamshell? Quick Answers for Packaging Buyers
- Protection and Shelf Appeal Are One Decision
What Is Thermoform Packaging?
Thermoform packaging is made by heating a flat plastic sheet until it softens, drawing it over or into a mold with vacuum or air pressure, cooling it so it holds the shape, and trimming the formed part from the web. Thin-gauge thermoforming produces most clear retail packs, including blisters, clamshells, trays and inserts.
Thermoform tooling costs less and arrives faster than injection mold tooling, which is why the process suits retail programs with many SKUs, seasonal runs and frequent artwork changes. The trade-off is less control over wall thickness. The sheet stretches as it forms, so some areas end up thinner than others, and much of good thermoform packaging design comes down to managing that stretch.
Blister, Clamshell, Trapped Blister or Skin Pack?
The format decides how the pack closes, how secure it is and how it looks on the hook. The most common retail option is thermoform blister packaging, where a formed plastic cavity is sealed to a printed paperboard backer card. A clamshell folds a single formed part around the product on a hinge, while a skin pack draws heated film tight over the product on a coated board, so it needs no product-specific mold at all.
| Format | How it closes | Security | Best for |
|---|---|---|---|
| Face-seal blister | Blister flange heat-sealed to the front of a coated card | Basic, a lifted edge shows tampering | Low-cost, high-volume items on peg hooks |
| Trapped or full-card blister | Blister flange held between two layers of board | Good to strong | Higher-value items that need better tamper resistance |
| Clamshell | One hinged part that snaps, seals or is welded shut | High, often needs scissors to open | Theft-prone electronics, tools and kits |
| Skin pack | Film drawn over the product onto a heat-seal coated board | Moderate | Irregular shapes and low volumes with no budget for a custom tool |
When teams compare blister vs clamshell packaging, the real question is how much security and protection the product needs for the unit cost you can carry. Face-seal blisters keep unit cost lowest, trapped and full-card designs add security at the price of more board, and clamshells give the most protection and theft resistance while using the most plastic. Skin packaging is worth a look when volumes are too low to justify a custom tool.
Start With the Product’s Weak Points
Start with a fragility map before anyone draws a cavity. Hold the product, shake it the way a parcel carrier might, and note where it could crack, scuff or scratch. Those vulnerable spots decide where the plastic should touch the product and where it needs to stand clear. Design the cavity outward from those contact points rather than inward from a standard pocket size.
Write the fragility map down alongside the other facts your thermoformer will ask for: product weight and dimensions with tolerances, finishes that mark easily such as gloss, chrome or soft-touch coatings, whether the item ships in parcels or on pallets, whether it hangs on a peg or sits on a shelf, and how the shopper is supposed to open it. Getting this on paper before the first supplier meeting saves rounds of samples later.
Think of the cavity as a cradle rather than a box. A snug cavity limits rattling, and that stillness often matters more than extra plastic. When the product cannot move, shock spreads across the formed shape instead of hammering one corner.
Design the Cavity: Draft, Radii and Draw Depth
Mold geometry provides most of the protection, and three features matter more than the rest.
- Draft angle. Sidewalls need a taper so the formed part releases from the tool. Female (cavity) molds need less draft than male (plug) molds, and many designers start around 3 to 5 degrees, adding more for textured surfaces and deep pockets. With too little draft, parts stick, scuff or tear on release.
- Corner radii. Generous radii spread loads instead of concentrating them along one sharp line, and they let the sheet flow more evenly. A common rule of thumb for thin-gauge packaging is an inside radius of at least 0.5 mm, and radii of 1 to 3 mm spread the material noticeably better.
- Draw depth. The deeper the pocket relative to its opening, the more the sheet stretches and the thinner the corners get. If the product is tall, consider laying it down, splitting it across two cavities, or using a clamshell so each half draws less deeply.
Ask your thermoformer which side of the part touches the tool. That surface holds dimension and finish, while the other side shifts with sheet thickness, so agree up front which faces control product fit and which control shelf appearance.
Put Thickness Where It Counts
Wall thickness works as both a budget and a safety factor. The aim is to keep enough material through corners and deep draws, with formed ribs adding stiffness where drops hit hardest. Flat panels and low-risk areas can stay thinner without weakening the pack’s main protective features. That cuts weight and material cost while the pack still feels solid in the hand, and well-supported corners stop it flexing while it hangs on a retail hook.
Retail blisters and clamshells are commonly formed from sheet around 0.25 to 0.75 mm thick (roughly 10 to 30 mil). That figure is the starting gauge, not the finished wall, and after forming the deepest corners can end up at a fraction of it. Specify a minimum wall thickness at the critical points as well as the sheet gauge, and ask for a sectioned first-off sample: cut through the deepest corner and measure it with a micrometer.
Tooling controls how that thickness is distributed. A well-designed mold, sometimes with a plug assist that pre-stretches the sheet, pulls material more evenly and reduces thinning around deep draws. When a prototype reveals a weak corner, a bigger radius or a step rib usually fixes it without moving the whole pack to heavier sheet.
Choose the Sheet: PET, RPET, PETG, PVC or PP
Clear PET is a common choice when shoppers need to see the product. It forms sharp detail and keeps a high-gloss face under store lighting. RPET packaging offers similar clarity with recycled content you can explain on the backer card, although tint and clarity can vary slightly between batches, so approve samples made from production material rather than a showroom swatch.
The PET vs PVC decision usually comes down to sealing and recycling. PVC is the most forgiving sheet to heat seal, while PET seals best to backer cards carrying a matched heat-seal coating. PETG sits between the two: it seals more easily than standard PET and can be RF-sealed, at a higher price. Polypropylene serves a different purpose. It is less clear than PET, but it resists many chemicals and tolerates impacts that can crack a stiffer clear sheet, which suits some hardware and chemical products.
| Sheet | Clarity | Sealing to card | Recycling notes | Typical use |
|---|---|---|---|---|
| PET (APET) | Excellent, high gloss | Needs a matched heat-seal coating | Resin code 1, though PET thermoforms are accepted in fewer programs than PET bottles | Electronics, cosmetics, premium retail |
| RPET | Very good, may show a slight tint | As PET | Resin code 1, with recycled content to communicate | Brands with recycled-content targets |
| PETG | Excellent | Easier than PET, RF-sealable | Carries code 1, but many PET recyclers treat it as a contaminant | Clamshells and RF-sealed packs |
| PVC | Good | Most forgiving | Resin code 3, rarely recycled and disruptive in PET recycling | Budget blisters, pharmaceutical blisters |
| PP | Translucent | Needs PP-compatible sealing | Resin code 5, recyclable where rigid PP is collected | Chemicals, hardware, hinged parts |
Ask for formed samples in at least two sheets, for example PET and RPET, or PET and PETG. Clarity, stiffness and surface feel are easier to judge in the hand than on a data sheet, and a sample sealed to your actual card stock tells you more than any specification.
Turn Protection Into Shelf Presence
The cavity that secures the product also presents it. Clarity carries much of the visual load, while the printed backer card carries the product information and branding. Keep copy flat on the card so it stays sharp. Text that runs under a curve distorts and becomes hard to read.
Steel-rule die cutting sets the card outline and hang hole, so plan both early alongside the blister shape. A clean seal between the blister flange and card creates a flat, tight edge that looks finished and resists peeling. Fit drives shelf presence: when the blister and card lines align and the product’s center of gravity sits under the hang hole, the pack hangs straight and reads clearly from several steps away. Keep barcodes in flat zones on the card, never behind curved plastic where glare and distortion can stop a scanner.
If you sell more than one SKU, design the pack as a family rather than a one-off. Shared flange sizes, card dimensions and hang-hole positions let new products launch on existing tooling and keep the range consistent on a peg wall. It is the same systems thinking behind how physical brand assets support scalable growth, applied to the structure of the pack as well as its graphics.
Build Security In From the Tool
Security works best when it is built into the tool rather than added late in development. Recessed flanges hide the seal edge and make signs of prying easier to spot. Tear notches give a controlled opening path and show whether the pack has been disturbed. Trapped and full-card blisters raise the bar further, because the flange sits between two layers of board instead of on the surface.
Clamshell packaging extends the same idea to higher-theft items. The product stays visible inside a formed shell that locks or seals around the edges and may need a cutting tool to open. That visibility supports shelf appeal while the sealed edge discourages quick removal. Match the lock to the retail setting, with hook-hang designs for peg walls and flat bases for shelf stacking. Keep the buyer in mind too: a pack that is almost impossible to open at home earns complaints and poor reviews, so add a tear strip or perforated opening path wherever the theft risk allows.
Medicines and household chemicals add another layer, because child resistance is regulated and has to be proven by testing. In the United States, child-resistant packaging is tested under the Poison Prevention Packaging Act protocol in 16 CFR 1700.20, and in Europe non-reclosable packs for pharmaceuticals are assessed against EN 14375. Bring a test lab in before the cavity and lidding are locked.
Prototype, Then Prove It With Transit Testing
Prototypes prevent expensive tooling changes. Form a short run on soft tooling made from wood, resin or a 3D-printed tool, then load the actual product and seal it using the intended production method. This shows where walls become too thin and where printed content drops out of view. Corrections at this stage are faster and cheaper than changes after aluminum production tooling is cut.
Blister pack testing should reflect the way the pack will actually travel. The ISTA test procedures give suppliers and buyers a shared language for this. 1-Series tests are quick integrity screens, 2-Series tests add elements such as atmospheric conditioning, and 3-Series tests simulate real distribution, with ISTA 3A covering individual packages sent through parcel networks and other 3-Series projects covering e-commerce fulfillment and direct imports. Drop sealed packs, vibrate them, apply stacking loads and condition them for the heat and humidity they will meet, then check for cracks, product damage and broken seals after each round.
Imported packs need extra attention. Sea freight from an overseas thermoformer can mean weeks inside a container that heats up and cools down every day, and those swings can curl backer cards and distort thin blisters. If your goods travel that way, condition test samples to match and agree on packing and transit terms with your logistics partner. Knowing exactly where freight forwarder duties start and stop makes it clear who answers for damage on each leg.
Finish with a retail check that labs often skip. Hang a batch of sealed packs on real peg hooks for several days and watch for card curl, flange lift and tilt. A pack that passes transit tests but sags on the hook still fails on the shelf.
Selling Online: When a Retail Pack Ships in a Parcel
A blister built for a peg hook was never meant to travel alone through a parcel network. When the same product sells online, the retail pack usually goes inside a mailer or shipping carton, and the features that sell it in store, such as the hang hole and the wide card, turn into crush points. Card corners fold, flanges lift, and the first thing the customer sees is a damaged pack.
Marketplaces add their own rules. Amazon’s Frustration-Free Packaging tier, for example, does not accept blister packs or welded clamshells and expects the customer to get the product out within 120 seconds, while its Ships in Own Container and over-boxing routes are tested against the ISTA 6-Amazon.com procedures. Check the current requirements before tooling, because a pack designed only for the hook may need a second format for online orders.
Many brands solve this with two formats: a blister or clamshell for retail, and a recyclable carton with a formed insert for ecommerce. The insert keeps the cradle idea from earlier in this guide without the card. Either way, how the pack arrives is part of the customer’s first impression, which is why packaging shows up among the trust signals in our guide to building E-E-A-T for direct-to-consumer brands.
Common Thermoform Packaging Failures and How to Fix Them
Most problems found at sample review trace back to a handful of causes. Use this table to diagnose them before anyone orders a new tool.
| Symptom | Likely cause | First fix to try |
|---|---|---|
| Cracked or split corners | Sharp radius, deep draw or sheet formed too cold | Increase the radius, reduce draw depth, review forming temperature |
| Blister peels away from the card | Heat-seal coating not matched to the sheet, or wrong seal time, temperature or pressure | Confirm coating compatibility with the sheet supplier and rerun seal trials |
| Product rattles in the cavity | Loose cavity or tolerances stacked the wrong way | Add contact ribs or tighten the cavity at the fragile points |
| Card curls or pack tilts on the hook | Humidity, light board or off-center weight | Use heavier board and move the hang hole over the center of gravity |
| Webbing between cavities | Cavities too close together or drawn too deep | Increase spacing on the tool or reduce cavity depth |
| Barcode fails to scan | Code printed under curved plastic or in a glare zone | Move the code to a flat area of the card |
| Scuffed product finish | Plastic rubs cosmetic surfaces in transit | Move contact points to non-cosmetic areas and add relief around finishes |
| Pack arrives crushed from online orders | Retail pack shipped without enough outer protection | Add an overbox or insert, or create a separate ecommerce format |
What Drives Thermoform Packaging Cost
Quotes vary a lot between thermoformers, but the same few variables sit behind almost every number. Knowing them makes it easier to compare suppliers and to see where a design change saves money.
- Tooling. Prototype tools are cheap and quick. Production tools are usually machined from aluminum and cost more, and the price climbs with the number of cavities, the depth of draw and details such as undercuts or hinges. More cavities cost more up front but lower the unit price at volume.
- Sheet. Material and gauge drive most of the unit cost once volumes are high, which is why moving the whole part to heavier sheet is the most expensive way to fix one weak corner.
- Card and print. Board grade, print colors, coatings and die-cut shape add cost on the blister side, and trapped or full-card designs use more board than face-seal cards.
- Sealing and loading. Heat sealing, RF sealing and hand loading each change the labor that goes into every pack.
- Runs and changeovers. Many SKUs on short runs cost more per pack than one SKU on a long run, which is another reason to share tooling across a pack family.
Ask each supplier to quote tooling and unit price separately, at two or three volume breaks, so you can compare like for like and see where the money goes.
Recyclability and the EU PPWR
Recyclable thermoformed packaging starts at the design stage. Mono-material packs recycle more easily than mixed ones, and a blister permanently bonded to a card is harder to sort than one the shopper can separate. Trapped blisters that slide out of the card, or face-seal designs with a perforated release, make separation easier. PVC remains the weak spot because it is rarely recycled and causes problems when it ends up in PET recycling.
In the European Union, the Packaging and Packaging Waste Regulation, Regulation (EU) 2025/40, has applied since 12 August 2026. It sets recyclability performance requirements and minimum recycled-content targets for plastic packaging that phase in from 2030, with harmonised material labels due from August 2028 or later. If you sell into the EU, start recording material composition and recycled content for every pack now, and expect hard-to-recycle formats to cost more as producer fees are adjusted for recyclability.
Whatever the market, keep claims on the card specific and provable. A recycled-content percentage your sheet supplier can document is useful to shoppers. A vague “eco-friendly” label with nothing behind it invites scrutiny from regulators and competitors alike.
What to Put in Your Thermoformer Brief
A one-page brief gets you better quotes and fewer sample rounds. Include:
- Product samples, CAD files or dimensions with tolerances, weight and the fragility map
- Format (blister, clamshell or skin pack) and display method: peg hook, shelf or both
- Sales channels: physical retail, your own online store, marketplaces or all three
- Preferred sheet and acceptable alternatives, plus any recycled-content target
- Minimum wall thickness at critical points, not only the starting gauge
- Seal method, backer card stock and heat-seal coating, so sheet and card are matched
- Security and opening requirements, including any child-resistance standard
- Shipping route and the ISTA procedure the pack must pass
- Annual volume, SKU count, launch date and the volume breaks you want quoted
Put artwork rules in the same brief: color references, logo zones, minimum type sizes and the flat areas reserved for barcodes. Packs produced by different suppliers drift apart quickly without them, and consistent visual branding is a large part of why shoppers trust one product over another on a crowded peg wall.
PET or PVC? Blister or Clamshell? Quick Answers for Packaging Buyers
A blister is a single formed cavity sealed or trapped against a printed backer card. A clamshell is one hinged formed part that folds around the product and snaps, seals or welds shut. Blisters usually cost less, while clamshells offer more protection and theft resistance.
PET gives better clarity and fits recycling systems far better, so it is the usual choice for consumer retail packs. PVC is cheaper and more forgiving to heat seal, but it is rarely recycled and can contaminate PET recycling. PETG is a middle option when sealing is the main concern.
It depends on the material and local collection. PET and PP packs are recyclable where those streams are collected, but PET thermoforms are accepted in fewer programs than PET bottles. Mono-material designs that separate easily from the card give a pack the best chance of being recycled.
Many retail blisters start from sheet around 0.25 to 0.75 mm (10 to 30 mil), with heavier gauges for large or heavy products. The finished wall at the deepest corners matters more than the starting gauge, so specify a minimum wall thickness at critical points and check it on sectioned samples.
Choose an ISTA procedure that matches the shipping route. ISTA 1A is a quick integrity screen, ISTA 2A adds conditioning and more realistic hazards, and ISTA 3A simulates individual packages moving through parcel delivery networks. Retailers and marketplaces may also set their own test requirements.
Yes, but not in every packaging program. Amazon’s Frustration-Free Packaging tier does not accept blister packs or welded clamshells, so many sellers ship the retail pack inside an overbox or use a carton with a formed insert for marketplace orders. Check Amazon’s current packaging requirements before you commit to tooling.
Not always. Stock clamshells and blisters suit standard product sizes, and skin packaging uses the product itself as the form, so no product-specific mold is needed. Custom thermoformed packaging pays off when volumes are steady, the product shape is unusual or the pack needs a distinctive shelf presence.
Protection and Shelf Appeal Are One Decision
Protection and shelf appeal stop competing when the design starts from the product’s requirements. Map the weak points, shape a cavity that holds the product still, choose a sheet that seals to your card and fits your recycling goals, then prove the result in transit, in the parcel and on the hook. Make those decisions before the production tool is cut, and the thermoform pack will protect the product through distribution and present it clearly wherever it is sold.
Standards and rules referenced in this guide:
- ISTA 1A, 2A, 3A and 6-Amazon.com test procedures, International Safe Transit Association
- 16 CFR 1700.20, the US Poison Prevention Packaging Act testing protocol for child-resistant packaging
- EN 14375, child-resistant non-reclosable packaging for pharmaceutical products
- Regulation (EU) 2025/40, the EU Packaging and Packaging Waste Regulation
- Amazon Frustration-Free Packaging certification guidelines
Last reviewed October 2026. Draft angles, corner radii and sheet gauges in this guide are common industry starting points, not specifications, so confirm them against your thermoformer’s tooling guidelines and your own test results, and check regulatory dates and marketplace rules against the official text before acting on them. Growwwth has no commercial relationship with Ultrapak or any other company linked in this article; the Ultrapak page is linked as an example of how a manufacturer presents the blister format.
